VariloVIMS

VIMS for production plants — safety that keeps up with the line

In manufacturing, risk is never abstract. It belongs to a specific machine, cell and shift. The problem is that knowledge about that risk spreads across the plant: maintenance keeps its inspection plan, engineering its modification files, and the safety team a spreadsheet of training dates. VIMS collects those threads around one object — the workstation and the machine — so a change in one place is visible everywhere else.

  • Machine park
  • Management of change
  • Chemicals and SDS
  • Exposure limits
  • Incidents and CAPA
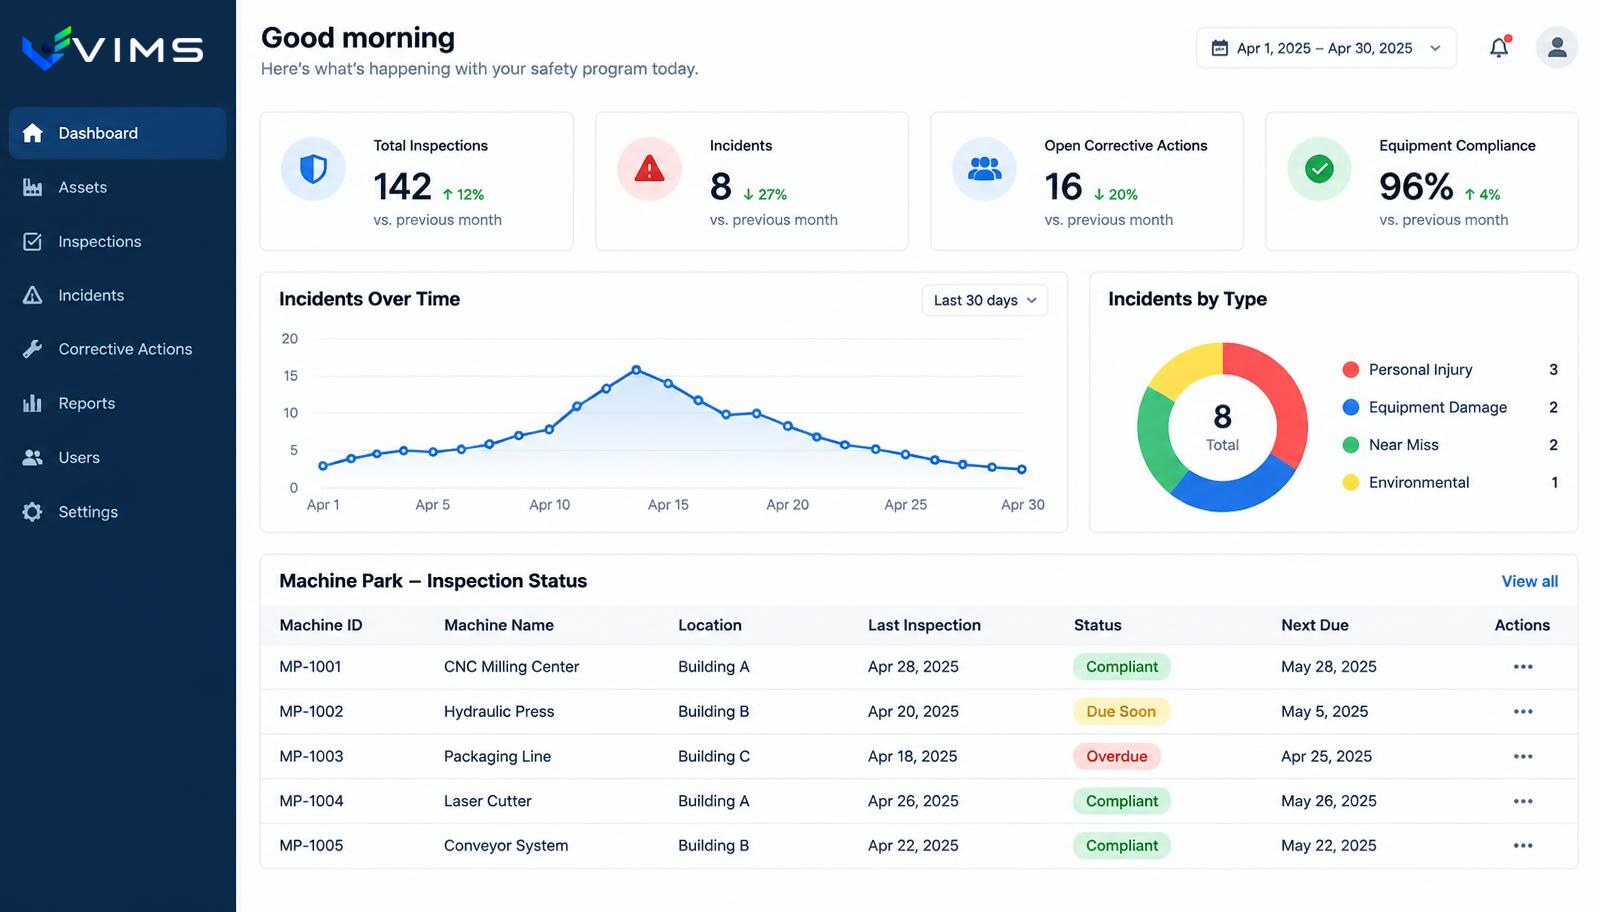
V-IMS — manufacturing dashboard: inspection count, open incidents and corrective actions, incident trend chart and a machine inspection status table with due dates

Why manufacturing loses safety data faster than other sectors

A production plant runs continuously, often across three shifts, and safety decisions are made at a pace that leaves no room for filling in spreadsheets. An operator mentions a leak to the shift leader, the shift leader passes it on during handover, and the information dies somewhere between a notebook and an inbox. Two weeks later nobody can reconstruct whether it was resolved.

The second mechanism is modification. A line rarely looks the way it did on handover day: a new feeder appears, a guard changes, someone relocates an emergency stop because it is more convenient. Each change looks minor on its own. Together they create a machine whose current risk assessment describes a state from three years ago.

The third is chemistry. In a plant with several hundred chemical items, a paper binder of safety data sheets stops being a register and becomes an archive. 'What exactly do we clean this line with, and what protection is required' then needs a phone call rather than a click.

What changes when data is attached to the technical object

VIMS treats the machine, the cell and the zone as first-class objects that everything else hangs from: the risk assessment, inspection history, reported issues, incidents, noise and dust measurements, the chemicals used at the station and the people holding the required qualifications.

The practical effect is simple. Opening the record of a hydraulic press, a maintenance manager sees not only the next inspection date but also the actions still open after the last incident and the change request waiting for its risk review. That picture needs no cross-referencing of three files.

The mechanism works both ways. When a measurement shows an exposure limit exceeded in the machining department, the system lists the stations and people working in that zone together with their health check and training status. 'Who is affected' stops being a query and becomes a view.

The features that work hardest in manufacturing

Machine park with history

A register of machines and equipment with inspection dates, reports, remarks and the actions arising from them — attached to the object, not to a separate spreadsheet.

Management of change

A request to modify a machine or process passes risk assessment and approval before it reaches the floor, and the decision trail stays with the object.

Chemicals tied to workstations

A substance list with safety data sheets plus where and in which process each is used, along with the protective equipment required.

Exposure monitoring

Workplace measurement results with exposure ratios and next survey dates, linked to zones and the employees they concern.

Reports raised from the floor

An operator reports an incident or near miss from a phone, with a photo and a location, without hunting for a form.

Cause – action – evidence chain

An incident leads to root cause analysis, analysis to actions with an owner and a date, and the action to confirmed effectiveness.

A typical flow in a production plant

From a signal on the floor to a confirmed technical change — every step leaves a trace on the machine it concerns.

  1. 1Report from the floor
  2. 2Assessment and triage
  3. 3Immediate containment
  4. 4Root cause analysis
  5. 5Change request
  6. 6Risk review of the change
  7. 7Implementation and briefing
  8. 8Effectiveness confirmed

Modules used in this industry

The starting set follows the processes that generate the most work and the most risk in this environment.

Registers and inspections

A plant runs a dozen parallel registers: cranes, pressure vessels, forklifts, extinguishers, hydrants, electrical installations, ladders, hoists, gates. Each has its own cycle and its own owner. This module brings them into one register with one calendar.

Explore the module

Management of Change (MOC)

Most serious events do not come from routine work but from something new: a replaced unit, an altered parameter, a different raw material, a reshuffled crew. MOC brings order to the moment when risk appears that no assessment describes yet.

Explore the module

VIMS module

One substance register, current safety data sheets available from a phone and full control over what is used where on site.

Explore the module

Workplace exposure monitoring

A measurement report usually goes into a binder and resurfaces at the next audit. Yet the result decides how often examinations are needed, what a referral must cover and what the risk assessment should say. This module turns a report into data you can use day to day.

Explore the module

VIMS module

Report an event in seconds, run the root cause analysis, plan actions and close the case with complete documentation in one place.

Explore the module

Root cause analysis

Repeating events usually mean the previous investigation stopped at human error. This module walks the team through structured RCA techniques and makes sure every finding becomes a concrete action.

Explore the module

VIMS module

No more action lists in a spreadsheet. Every action has an owner, a deadline, a status and an effectiveness check — all in one view.

Explore the module

Rounds and inspections

A safety walkaround is a cheap prevention tool, but only when it happens regularly and ends with an assigned task. This module enforces both conditions.

Explore the module

Three shifts, one picture of the plant

Shift work creates a specific information risk: the same machine has three operators a day and three versions of knowledge about its condition. A report made at 23:40 must be visible to the morning shift regardless of whether anyone mentioned it verbally.

In VIMS, reports, walks and inspections land in a shared event stream for the object and become the natural content of a shift handover. The shift leader no longer needs a private notebook, because the notebook is a view filtered by area and date.

Frequency adds value. If the same type of report appears every week on the same machine, that pattern is visible without manual analysis — usually the moment a small defect stops being a defect and becomes a candidate for a permanent technical change.

How rollout looks in a plant that is already running

The first step is rarely risk assessment. It is registers: employees, workstations, machines and zones. Without them every later module works on free text and no meaningful report can be built from it afterwards.

The second step is usually the simplest input stream — reports and safety walks. They produce a quick, visible result for the crew and build the habit of using the system on a phone before more formal processes arrive.

The third stage covers processes that need discipline: incidents with root cause analysis, corrective actions and management of change. Starting there is tempting, but without base data it ends with typing the same names and machines again.

Questions from production plants

Does VIMS suit a plant with several hundred machines?

Yes. The object register is hierarchical, so machines can be organised into departments, lines and cells, and inspections, incidents and actions can be filtered along that structure.

Does an operator need an account to report an issue?

Access scope is set by the organisation. A common model is an employee account with a limited view covering reports and personal documents, with no access to other people's HR data.

How does the system handle machine modifications?

A modification is a separate process: request, risk assessment, approval and implementation. The machine file keeps a record of who allowed the change and on what basis.

Can we keep a chemical register with safety data sheets?

Yes, including assignment of substances to stations and processes, so the list of protective measures reflects actual use rather than a warehouse catalogue.

Does rollout require stopping current procedures?

No. Rollout is usually staged: registers and reports first, then inspections, then processes that need approvals. Existing documents can be migrated gradually.

Other industries

Industry: food industry and FMCG

See

Industry: logistics, warehousing and distribution

See

Industry: construction and contracting

See

Industry: multi-site organisations

See

Industry: EHS consultancies and outsourced safety services

See

See VIMS mapped onto your plant

We will show a flow built on your departments, machines and shift pattern rather than a generic demo.